China Model 200 Single-Axle Flatbed Trailer Factory Manufacturing Processes and Quality Control
2026-09-18
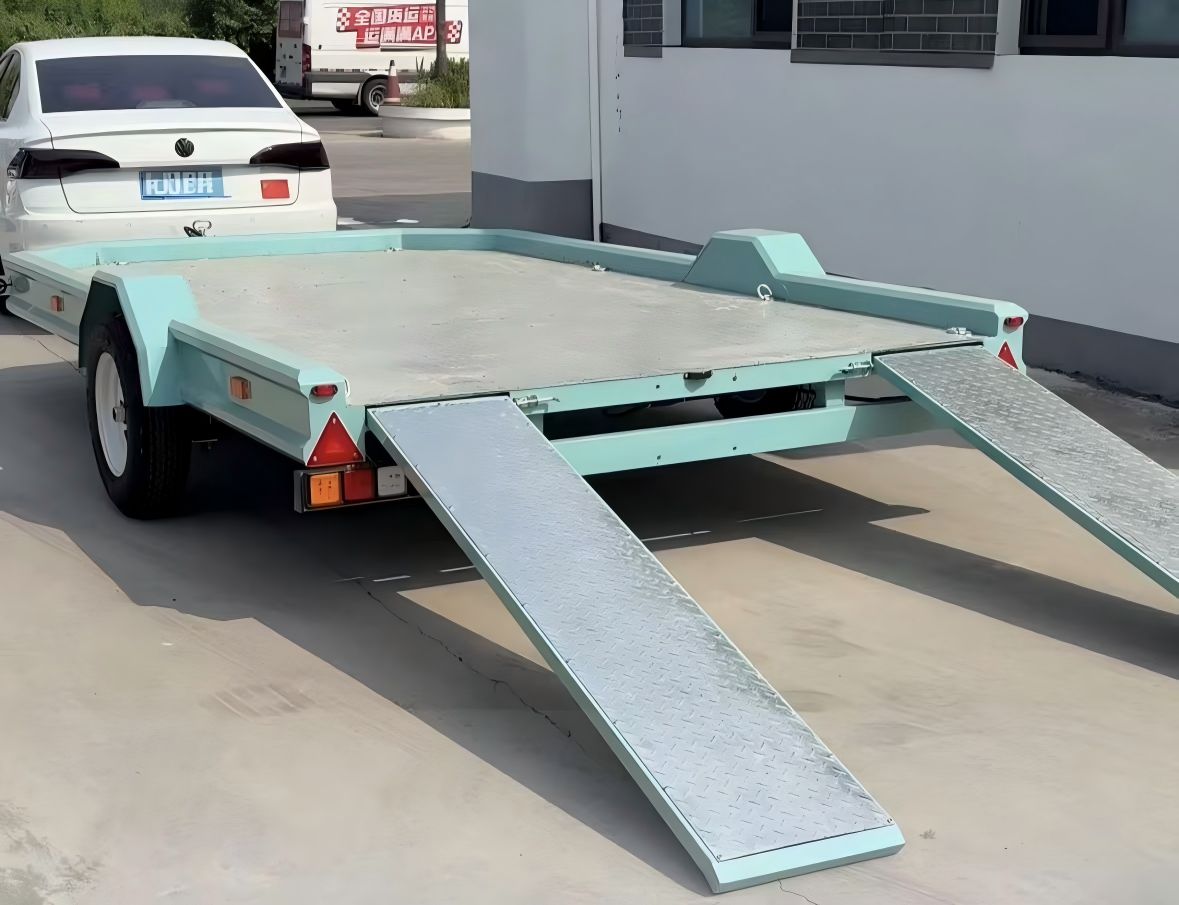
The first thing you notice about a Model 200 single-axle flatbed trailer rolling off a Chinese production line isn't the hum of machinery or the sharp smell of fresh paint—it's the near-surgical rhythm of each station. At Whole Chain Tech, that rhythm isn't accidental. It comes from a manufacturing process where every weld is mapped, every torque value logged, and every batch of steel traced back to its mill. Quality control here doesn't mean a final walk-around; it means rejecting a frame for a 0.3-millimeter deviation most factories wouldn't even measure. So what actually separates a trailer built to survive rough terrain from one that just looks the part? That's the question this post unpacks, station by station.
Incoming Steel: What Gets Unloaded Only After Certification
Steel shipments don't simply roll off the truck because they've arrived. Every incoming bundle, plate, or coil sits on the trailer until the receiving team verifies that the accompanying material certificates match the heat numbers stamped on the steel itself. That cross-check—between paperwork and physical markings—is the first gate. If a single digit is off, the load stays put.
Beyond the paperwork, dimensional checks and visual surface inspections happen before the crane gets involved. A quick look for deep pitting, lamination, or edge damage can save hours of rework later. Only after the QC lead signs the delivery note does the unloading crew begin moving steel into the designated quarantine zone, where it waits for any additional lab testing the project specs demand.
This isn't bureaucratic delay; it's the difference between catching a nonconforming heat at the gate and discovering it after it's already cut and welded into place. Once steel is buried in an assembly, tracing it back to a supplier is costly. Certification first keeps the problem outside the shop floor.
Cutting and Forming the Main Beams Without Heat Distortion
Main beams are rarely forgiving once heat enters the equation. A cutting torch lingering too long on one side of a flange or web can leave a permanent bow that no amount of clamping will pull out later. We sidestep this by using cold saws or high-speed band saws for the initial severing, and when thermal cutting is the only option, we keep the plasma arc fast and tight while a water-cooled copper bar sits clamped directly behind the cut line. The chill strip pulls heat away before the steel can expand unevenly, leaving the cut edge straight and the beam’s camber untouched.
Forming the beams without heat is more about sequence than force. Rather than heating a stubborn camber into place, we set up a three-point press with sacrificial shims at the load points and work in short, incremental strokes along the length. Between passes the beam is allowed to rest and spring back on its own, then we check residual bow with a taut wire instead of relying on a single dial indicator. This slow, cold-working rhythm keeps flange tips from curling and prevents the web from oil-canning under uneven stress.
Where some shops still reach for a rosebud tip to correct small misalignment, we prefer mechanical straightening with controlled over-bend. If a beam comes off the rolls with a slight twist, we clamp the high corner and use a hydraulic ram to push past yield in the opposite direction, holding it for a few minutes before release. The correction is checked at multiple stations, never just at midspan, because heat-free forming tends to reveal its errors at the ends first.
Jig Welding the Frame: Every Pass Checked Before It Cools
Once the first bead goes down on a frame corner, the jig doesn't get a break. The welder stops, grabs a square and a straightedge, and checks the critical dimensions while the steel is still radiating heat. That's the whole point of "every pass checked before it cools." A hot weld is far more willing to move—tap it, clamp it, or pull it back into line without cracking. Wait until the bead has cooled, and any distortion is already locked into the frame, which means cutting, grinding, and starting over.
This isn't just about catching mistakes. The sequence matters as much as the inspection. A long pass along one side will pull the opposite rail out of parallel, so the welder alternates corners and keeps the heat input low enough to check between passes. The jig itself takes a beating too—clamps get repositioned, shims get swapped, and the frame gets a hard look after every single weld. It's slower, but it beats finding a 3/16-inch twist after the whole assembly has cooled.
The Anti-Corrosion Line: Shot Blast to Final Topcoat
The backbone of any durable coating system lies in how well the surface is prepared before the first layer goes on. Shot blasting strips away mill scale, rust, and old coatings, leaving a clean, angular profile that gives the primer something to bite into. Without that mechanical anchor, even the best topcoat will eventually lose its grip, blister, and fail long before its expected service life.
From the blast booth, the work moves through a series of controlled steps: primer application to lock out moisture, intermediate coats to build film thickness and add barrier protection, then the final topcoat for UV resistance, chemical tolerance, and the required finish. Each stage has its own cure window and humidity tolerance, and skipping or rushing any one of them shows up later as edge creep, pinholing, or underfilm corrosion.
Quality control along the line means checking profile depth, dry film thickness, and adhesion at key points, not just at the end. When the topcoat finally goes on, it should be the predictable result of everything that came before it—not a last-minute fix for a poorly prepared substrate. That sequence, from abrasive impact to final gloss, is what separates a coating that lasts a decade from one that needs touch-ups in the first year.
Suspension and Axle Mounting: Torque Marks Tell the Story
When you slide under a truck or trailer for a routine inspection, the suspension and axle mounting hardware rarely gets the attention it deserves—until something loosens. Torque marks, those small paint lines bridging bolt heads to their mounting surfaces, are the fastest way to spot movement before it becomes a roadside failure. A clean, unbroken line means the fastener hasn't rotated since it was torqued. But a crack in the paint, or a line that no longer aligns, tells you the joint is working against itself.
Checking these marks doesn't require special tools, just a flashlight and a willingness to look past the obvious. Run your finger along the mark if you can reach it; often you'll feel a step or misalignment before you see it. Keep in mind that torque marks are a visual aid, not a replacement for scheduled torque checks. They will catch rotation, but they won't tell you if a bolt has stretched or lost clamping force without moving. So treat a broken mark as a trigger to grab the torque wrench and verify the actual spec—especially on U-bolts, control arm bolts, and axle flange fasteners where loads shift constantly.
After re-torquing or replacing hardware, reapply the mark properly. Use a paint pen or torque seal that dries brittle, not a soft grease pencil that smears. The mark should jump from the bolt head onto the adjacent stationary surface in a single straight line, so any movement is obvious at a glance. And don't paint over an old mark without cleaning the surface first; otherwise you're just hiding the evidence. A disciplined marking routine costs minutes but saves you from chasing mystery clunks, uneven tire wear, and the kind of failures that happen at the worst possible moment.
Final Roll Test: Simulated Loads Before the Serial Plate Goes On
The last physical check before a roller receives its serial plate is a deliberately harsh one. A dedicated bench applies a series of programmed radial and axial loads that mirror the worst-case forces the part will see in the field, from cold-start torque spikes to sustained high-speed operation. This is not a simple spin-up; the roller is pushed through rapid load reversals and brief overload conditions, all while sensors track deflection, temperature rise, and any sign of surface distress.
What makes this stage different from earlier inspections is the level of realism. The simulated loads are derived from actual customer duty cycles, adjusted for a safety margin that sits just inside the design envelope. Technicians watch for micro-slippage at the contact patch, listen for harmonic changes that suggest subsurface fatigue, and measure runout with a laser after each load block. If the roller survives the full sequence without breaching any tolerance, it is deemed ready for final marking.
Passing this test means more than meeting a spec sheet — it confirms that the heat treatment, grinding, and assembly steps have come together correctly under stress. Only then is the serial plate attached, turning a tested component into a traceable, ship-ready unit. A failure here is rare but valuable: it points to a process drift that might have gone unnoticed until it reached a customer's machine.
FAQ
The main beams and cross members are cut from Q235 or Q345 structural steel, depending on the load rating. We use laser-cut plates and cold-formed channel sections to keep the frame straight and reduce warping during welding.
The deck is laid over the cross members and secured with countersunk bolts or plug welds, not just perimeter tack welds. We also apply a bead of polyurethane sealant between the deck and frame to stop moisture from getting trapped and causing rust.
Most of the frame is welded with MIG (GMAW) using mixed gas to get deeper penetration and less spatter. Critical joints, like the coupler plate and spring hangers, are done by certified welders and checked with a weld gauge.
After welding, the whole frame goes through shot blasting to remove mill scale and weld slag. Then it gets a zinc-rich primer, followed by two coats of polyurethane topcoat. This gives the trailer a smooth finish and better resistance to stone chips.
We use a laser alignment tool to measure from the kingpin or coupler center to each end of the axle. The tolerance is kept within ±2 mm. If it is out, we adjust the spring seat position before final torque.
Each trailer is loaded to 125% of its rated capacity on a test bed and inspected for cracks or deformation. We also do a road test with a loaded trailer over speed bumps to check for rattles, brake pull, and loose hardware.
Yes, we offer deck lengths from 2.4 m to 4.5 m and can add removable side rails, stake pockets, or a front tool box. The frame design is modular, so these changes do not require retooling the jigs.
Fully assembled trailers are shrink-wrapped and placed on steel stands in a 40 ft container. For bulk orders, we can knock down the trailer into frame, axle, and deck bundles to save freight space. All parts are labeled with assembly drawings.
Conclusion
At the China Model 200 single-axle flatbed trailer facility, nothing reaches the cutting station until the incoming steel has been verified against its mill certificates—chemistry, thickness, and surface condition are checked at the gate, not after the fact. Main beams are then cut and formed with sequenced torch travel and controlled cooling so the heat-affected zone stays tight and straight; you won't see wavy flanges or hard spots that show up later as cracks. The frame moves into jig welding, where every pass is inspected while the weld is still warm, allowing immediate correction instead of waiting for a batch teardown.
From shot blasting to the final topcoat, the anti-corrosion line runs as a single continuous process, with dry-film thickness and adhesion recorded at fixed intervals rather than sampled at the end. Suspension and axle mounting rely on torque markings that let any inspector read the tightening history at a glance, so a missed fastener cannot hide. Only after a final roll test applies simulated load cycles—bouncing the empty deck, checking alignment under load, and listening for creaks—does the serial plate get riveted on. That sequence is deliberate: the plate is not a starting point, it is proof the trailer survived the same checks that the factory's own warranty depends on.
Contact Us
Contact Person: Ethan
Email: [email protected]
Tel/WhatsApp: +86 13963964935
Website: https://www.wholechaintech.com/